Ball Nose Finishing in Mold Steel: Stepover, Scallop and Tool Life
The stepover you choose decides three costs at once: polish time, tool life and delivery date. A practical method for mold work in P20 and 2344.
In mold work, the ball nose end mill is the last tool to touch the cavity — which means it is also the last place to save time. The trade most shops make is stepover versus polishing hours. The trade they forget is stepover versus tool life.
Scallop height: the arithmetic you actually need
Scallop height falls off with the square of stepover. Halve the stepover and the cusp drops to roughly a quarter. That is why dropping from 0.30 mm to 0.15 mm stepover with a R6 ball nose takes the residual from “hand polish for half a shift” to “stone and be done”.
| Tool | Stepover | Scallop height | Practical finish |
|---|---|---|---|
| R6 ball nose | 0.30 mm | ~1.9 µm | Hand polish required |
| R6 ball nose | 0.15 mm | ~0.5 µm | Light stone finish |
| R6 ball nose | 0.08 mm | ~0.15 µm | Near-polish as machined |
The tool-life side of the trade
Fine stepover means the effective surface speed at the contact point stays high while radial engagement drops. Two rules keep the edge alive:
- Run the speed the nose can take. At small stepovers the contact point migrates toward the tool tip on steep walls, where surface speed collapses. Keep RPM high enough that the nose is still cutting, not burnishing.
- Do not baby the feed. A ball nose run too lightly rubs, work-hardens the surface, and then chips when it finally bites. In P20, 180–220 m/min with 0.05–0.08 mm/z per tooth equivalent is a stable window.
Geometry details that matter in mold steel
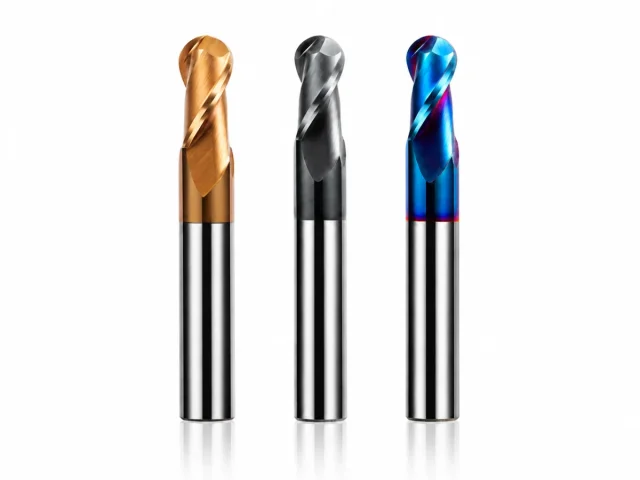
A finishing ball nose for 2344 / H13 should be ground with a sharp polished edge — no heavy hone — and a core that is strong enough for the tool to be used to the full-flute depth when the CAM link demands it. Coating: AlTiN at 3 µm handles the dry-or-MQL finishing pass; bright uncoated still has its place for the final spring pass in big cavities where smear is the enemy.
We grind mold-finishing ball nose tools to drawing, from R0.5 up. See the ball nose family or send the cavity specification.