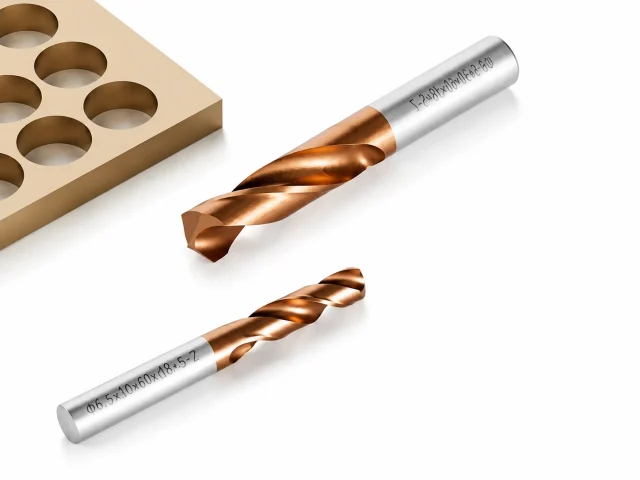
Solid Carbide Drill 3×D — Standard
The everyday carbide drill for holes up to three diameters deep. Faster than HSS, and it holds size.
Ø1–20 mm · 2 (140° point) · TiAlN
Eight product families covering milling, drilling, reaming and deburring — with custom geometry ground to your drawing.
The everyday carbide drill for holes up to three diameters deep. Faster than HSS, and it holds size.
A long, slender ball nose for deep cavities and radii that sit well below the surface line, with a tapered…

The standard-length ball nose: the everyday tool for 3D surfacing, radius blending and finishing in a rigid setup.

Four flutes for high-feed finishing in hardened tool steel, with an AlTiN coating that survives the heat.
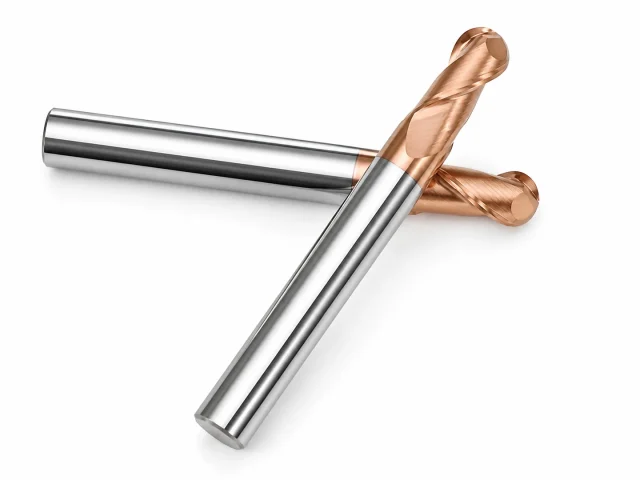
A half-degree taper lets one tool finish drafts, fillets and deep ribs that would otherwise need three setups.
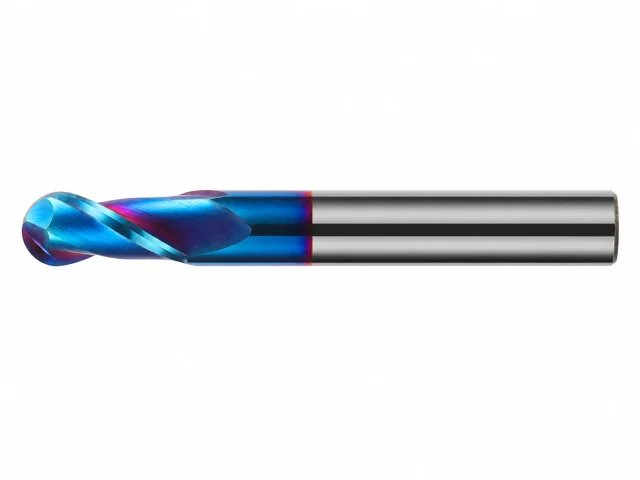
Neck relief and a four-flute core for cavities deeper than three diameters, where chip evacuation and stiffness both matter.
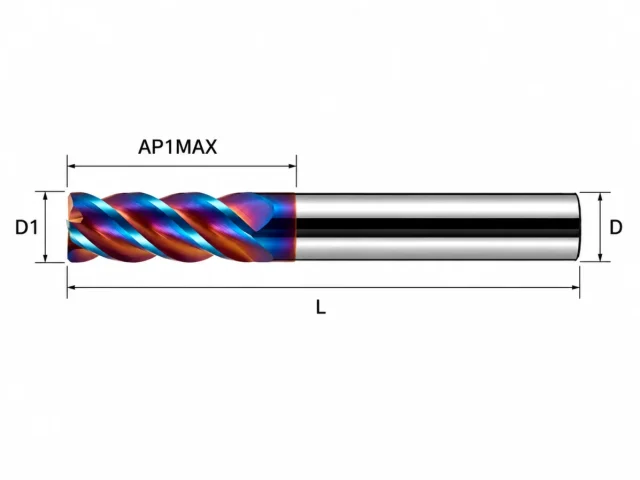
Variable helix and unequal flute spacing break the harmonics that make stainless steel ring. Quieter, and noticeably longer tool life.
A radius at the corner makes the edge last. Variable helix keeps it quiet. The tool most shops settle on…
A fixed 0.5 mm radius corner, ground to ±0.01 mm, for production work where the radius is specified on the…

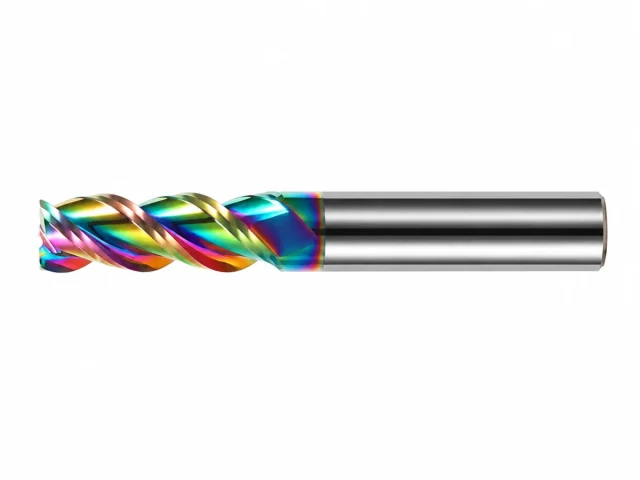
High-helix three-flute geometry with a radiused corner for aluminium, where chip clearance decides the finish.
Six flutes, a generous radius and a strong core for high-feed roughing strategies where the machine can take it.
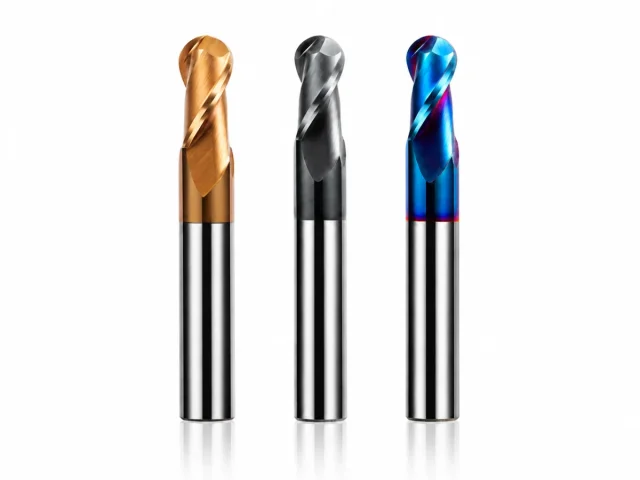
For the top of the hardness range: an ultra-fine substrate and AlTiN coating that keep cutting where standard grades stop.
Most of what we ship is ground to a drawing. Send yours — we quote within 24 hours.