About this tool
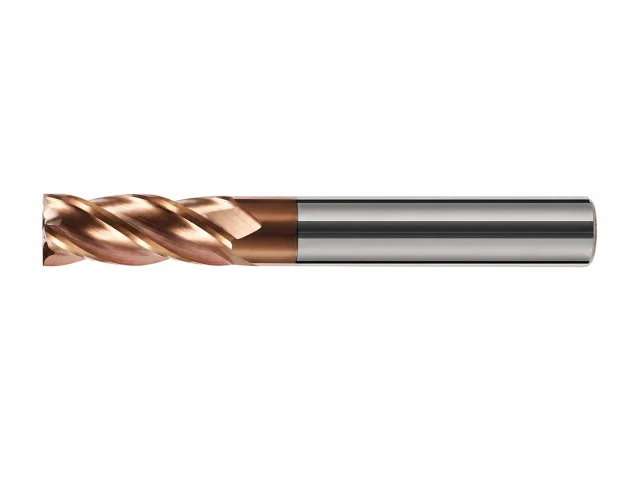
Above 55 HRC the failure mode changes: the edge does not wear out so much as break down. An ultra-fine substrate and a reinforced land keep the radius intact long enough to finish the job, which is what you actually pay for at this hardness.
Where it works
Finishing dies, molds and tooling in 55 to 62 HRC steel. Light depths of cut, high spindle speed, and a rigid setup.
Cutting data — starting point
Starting values for a rigid setup with a good coolant supply. Treat them as a first trial, then adjust to the machine, the holder and the actual condition of the material.
| Work material | Cutting speed vc | Feed | Depth of cut |
|---|---|---|---|
| Hardened steel 55–62 HRC (H) | 70–110 m/min | 0.008–0.025 mm/tooth | 0.15×D |
| Hardened steel 62–65 HRC (H) | 50–80 m/min | 0.006–0.018 mm/tooth | 0.1×D |
What you can specify
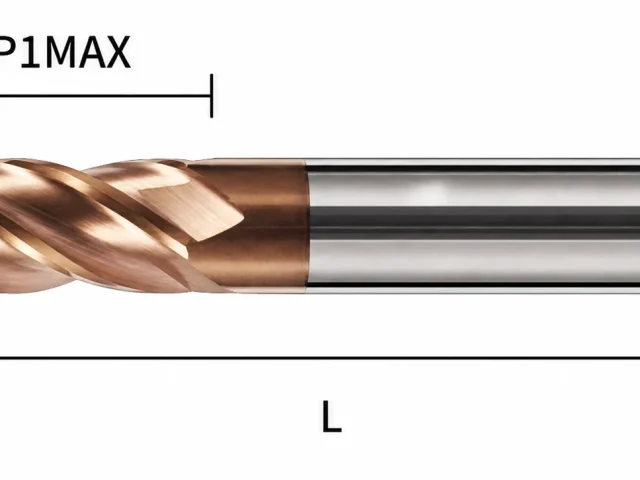
- Diameter, corner radius and flute count ground to your drawing
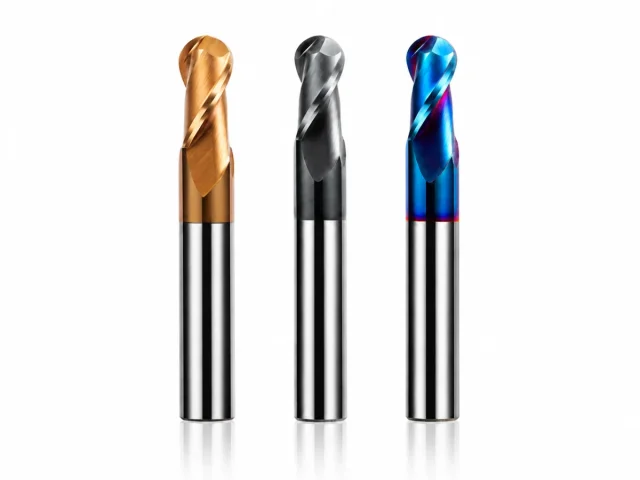
- Coating — AlCrN, AlTiN, TiAlN, DLC or uncoated, matched to the workpiece
- Shank — h6 ground, HA / HB / whistle-notch
- Laser-marked part number, or blank shanks for distributor stock
Not sure about the geometry? Send the drawing or a photo of the part. We recommend the profile, the coating and the starting cutting data — and quote from there.