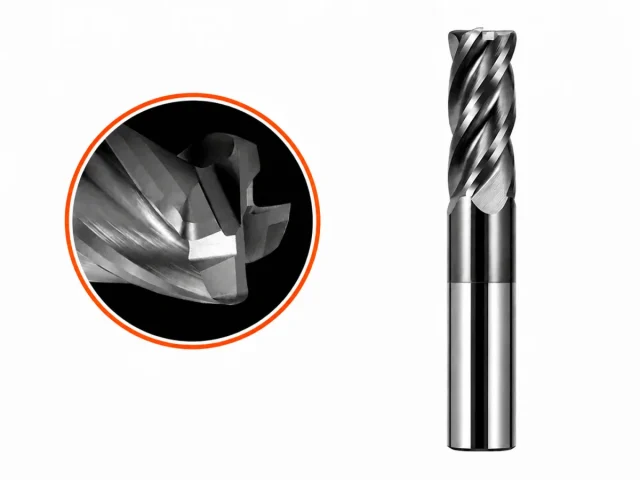
About this tool
Stainless steel is where ordinary end mills start to sing. Unequal flute spacing and a variable helix change the frequency at which the tool and the workpiece vibrate, which means a quieter cut, a better surface and far fewer chipped edges.
Where it works
Austenitic and duplex stainless steels, superalloys and titanium. Particularly effective on long-reach setups where rigidity is limited.
Cutting data — starting point
Starting values for a rigid setup with a good coolant supply. Treat them as a first trial, then adjust to the machine, the holder and the actual condition of the material.
| Work material | Cutting speed vc | Feed | Depth of cut |
|---|---|---|---|
| Stainless 304/316 (M) | 80–130 m/min | 0.02–0.05 mm/tooth | 0.3×D |
| Duplex stainless (M) | 60–100 m/min | 0.015–0.035 mm/tooth | 0.25×D |
| Titanium (S) | 50–90 m/min | 0.015–0.030 mm/tooth | 0.2×D |
What you can specify
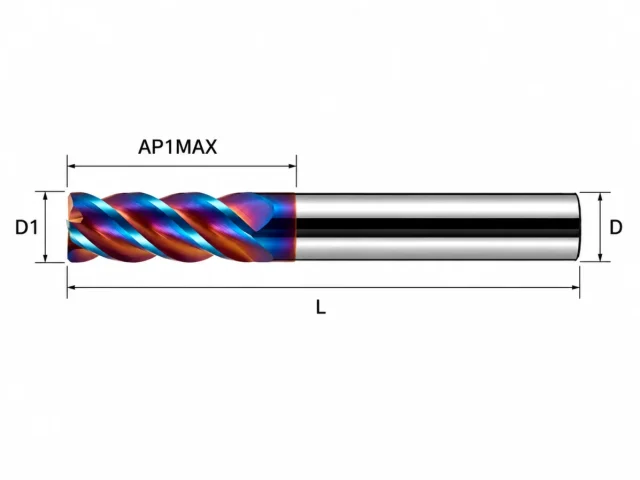
- Diameter, corner radius and flute count ground to your drawing
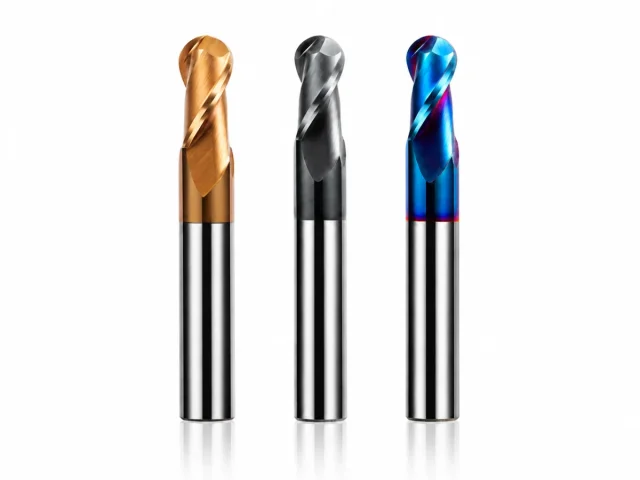
- Coating — AlCrN, AlTiN, TiAlN, DLC or uncoated, matched to the workpiece
- Shank — h6 ground, HA / HB / whistle-notch
- Laser-marked part number, or blank shanks for distributor stock
Not sure about the geometry? Send the drawing or a photo of the part. We recommend the profile, the coating and the starting cutting data — and quote from there.