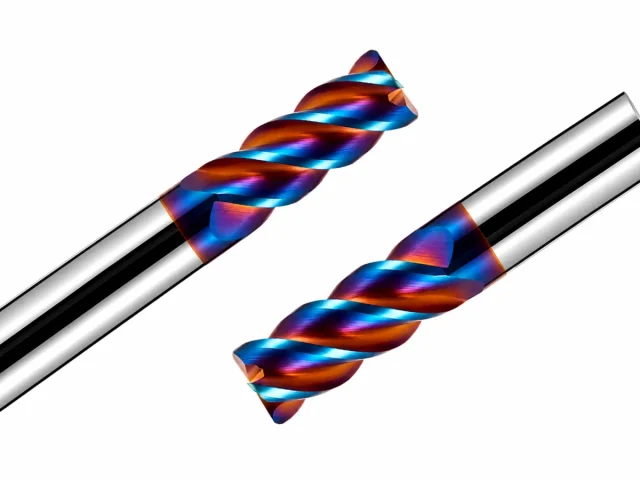
About this tool
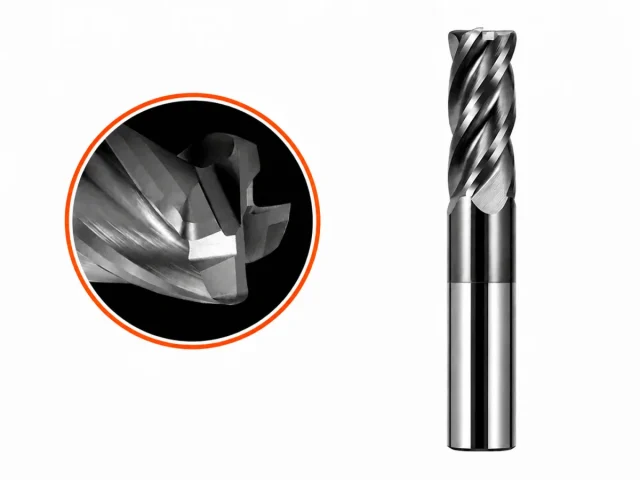
Three flutes and a deep, polished chip gullet — the geometry that stops aluminium from welding to the edge. Run it hard: this tool is designed for high spindle speeds and generous feed rates.
Where it works
Aluminium and other non-ferrous materials, plastics and composites. Ideal for profile cuts, slots and pockets where chip evacuation is the limit rather than the tool.
Cutting data — starting point
Starting values for a rigid setup with a good coolant supply. Treat them as a first trial, then adjust to the machine, the holder and the actual condition of the material.
| Work material | Cutting speed vc | Feed | Depth of cut |
|---|---|---|---|
| Aluminium (N) | 300–600 m/min | 0.05–0.12 mm/tooth | 0.5×D |
| Aluminium 7075 (N) | 250–450 m/min | 0.05–0.10 mm/tooth | 0.4×D |
| Plastics (N) | 200–400 m/min | 0.05–0.10 mm/tooth | 0.5×D |
What you can specify
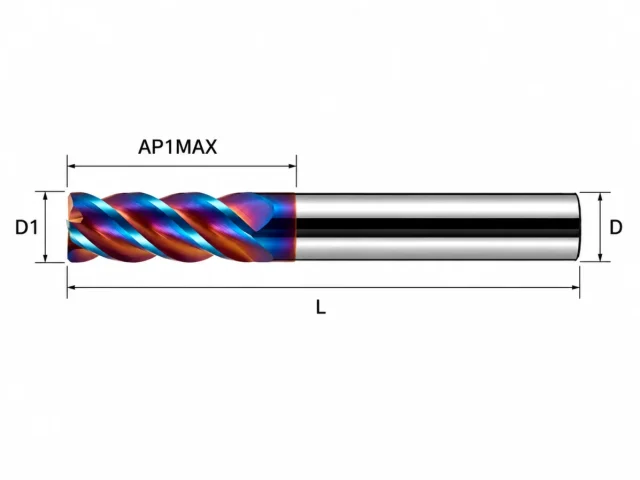
- Diameter, corner radius and flute count ground to your drawing
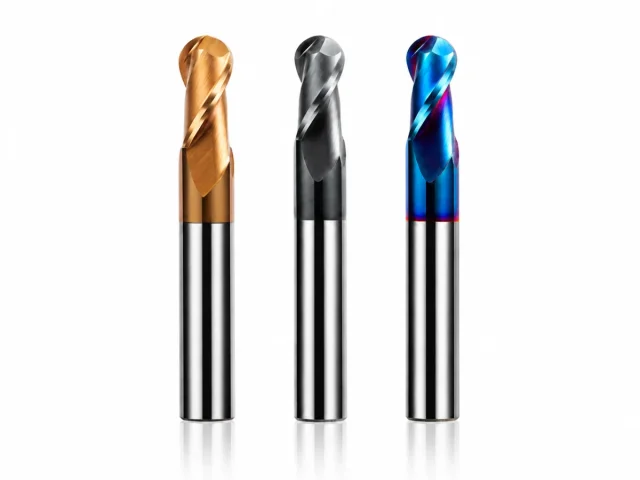
- Coating — AlCrN, AlTiN, TiAlN, DLC or uncoated, matched to the workpiece
- Shank — h6 ground, HA / HB / whistle-notch
- Laser-marked part number, or blank shanks for distributor stock
Not sure about the geometry? Send the drawing or a photo of the part. We recommend the profile, the coating and the starting cutting data — and quote from there.