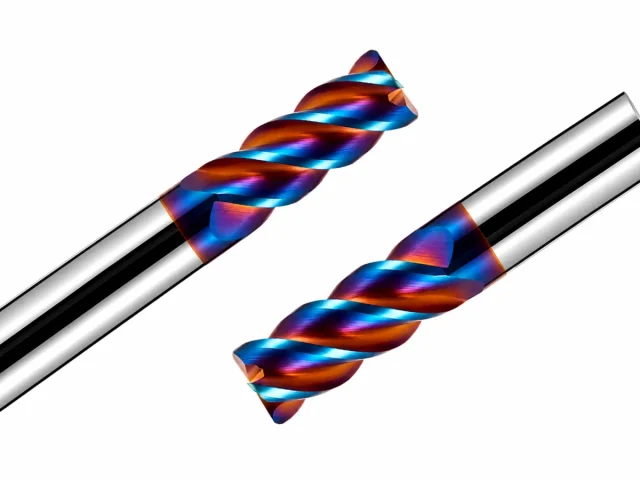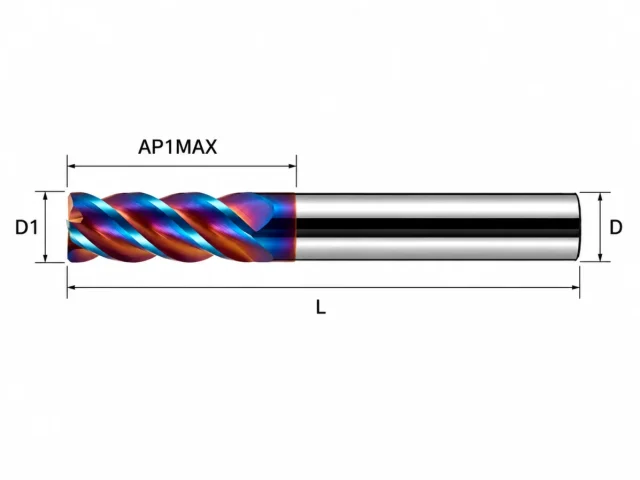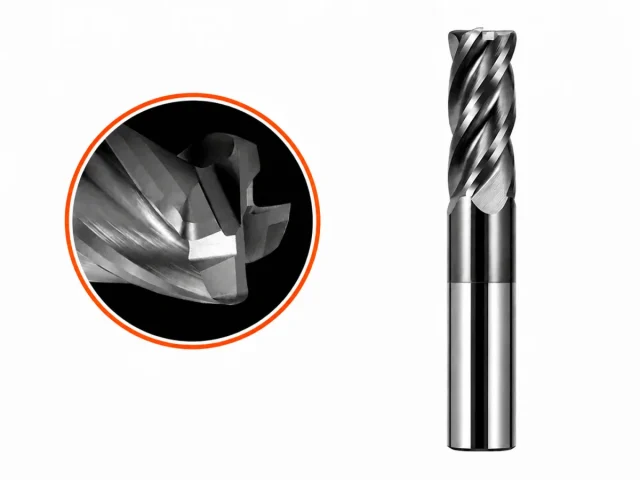
About this tool
When the roughing is done and the surface has to come out right the first time, six flutes give you the feed rate to finish quickly without pushing the chip load up. The stiffer core also holds the wall straighter on deep passes.
Where it works
Finishing passes in steel, cast iron and hardened steel up to 55 HRC. Best where the machine has the spindle speed to keep the chip load in range.
Cutting data — starting point
Starting values for a rigid setup with a good coolant supply. Treat them as a first trial, then adjust to the machine, the holder and the actual condition of the material.
| Work material | Cutting speed vc | Feed | Depth of cut |
|---|---|---|---|
| Carbon steel (P) | 200–300 m/min | 0.02–0.05 mm/tooth | 0.3×D |
| Hardened steel 45–55 HRC (H) | 90–140 m/min | 0.01–0.025 mm/tooth | 0.15×D |
| Cast iron (K) | 180–260 m/min | 0.02–0.04 mm/tooth | 0.3×D |
What you can specify
- Diameter, corner radius and flute count ground to your drawing
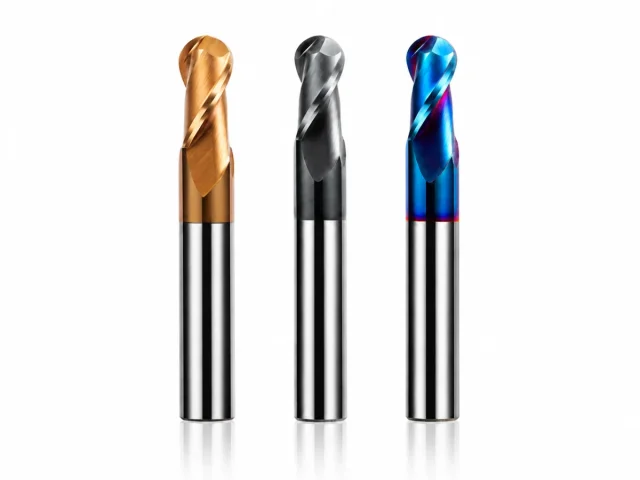
- Coating — AlCrN, AlTiN, TiAlN, DLC or uncoated, matched to the workpiece
- Shank — h6 ground, HA / HB / whistle-notch
- Laser-marked part number, or blank shanks for distributor stock
Not sure about the geometry? Send the drawing or a photo of the part. We recommend the profile, the coating and the starting cutting data — and quote from there.