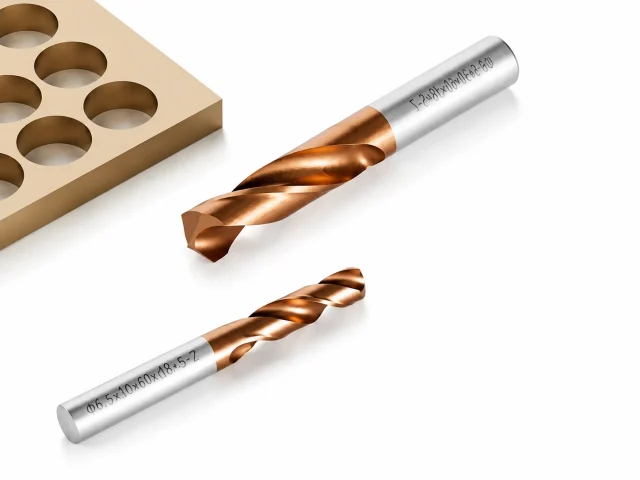
Solid Carbide Drill 3×D — Standard
The everyday carbide drill for holes up to three diameters deep. Faster than HSS, and it holds size.
Read more
The everyday carbide drill for holes up to three diameters deep. Faster than HSS, and it holds size.
Read more
Four flutes for high-feed finishing in hardened tool steel, with an AlTiN coating that survives the heat.
Read more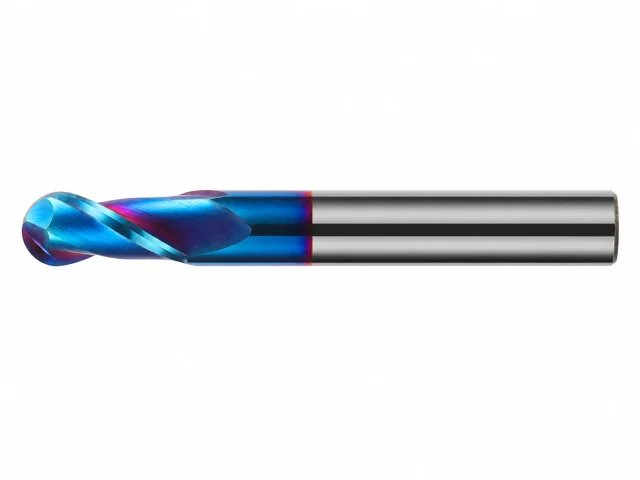
Neck relief and a four-flute core for cavities deeper than three diameters, where chip evacuation and stiffness both matter.
Read more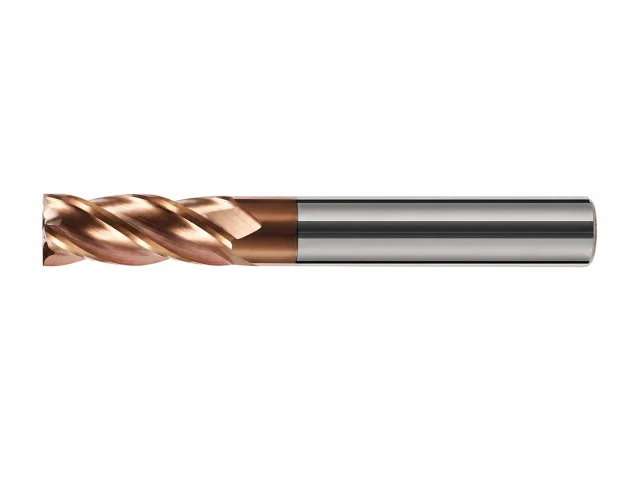
A fixed 0.5 mm radius corner, ground to ±0.01 mm, for production work where the radius is specified on the drawing.
Read more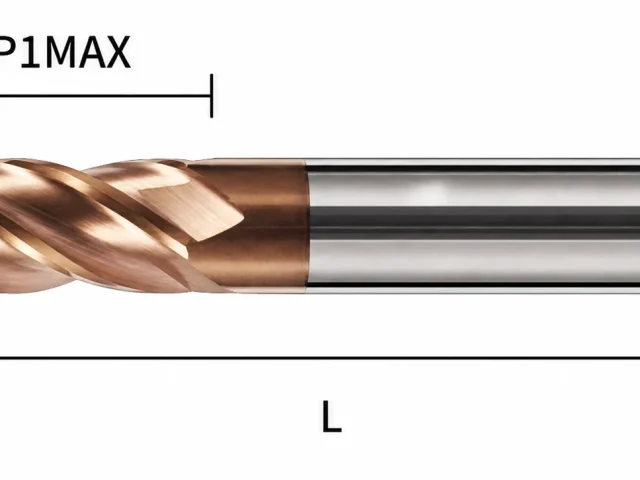
Six flutes, a generous radius and a strong core for high-feed roughing strategies where the machine can take it.
Read more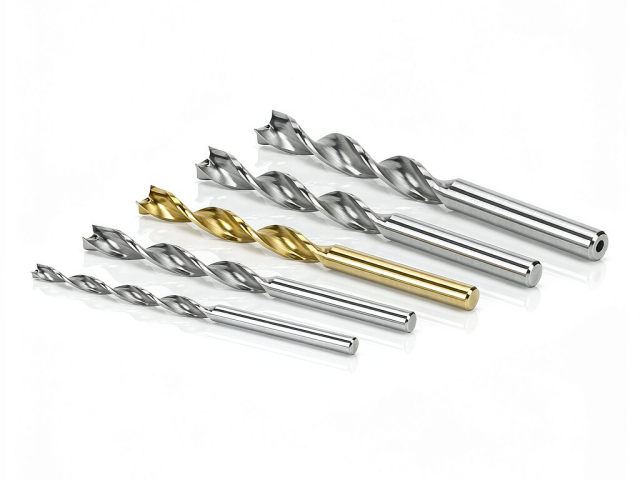
Five diameters deep with coolant straight to the tip. The drill that makes deep holes routine in steel and stainless.
Read more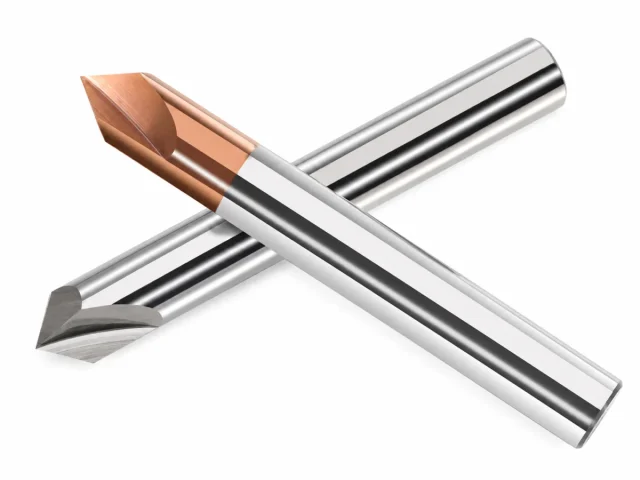
Eight diameters, internal coolant and a strengthened web: for the holes that normally need a gun drill and a second operation.
Read more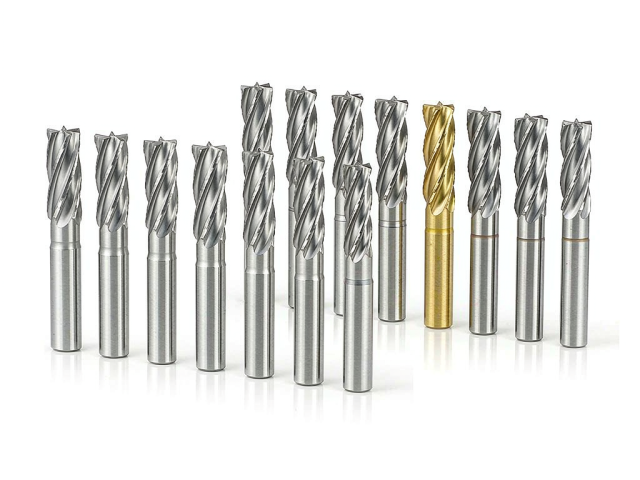
Six flutes and a ground H7 tolerance for holes that have to come out on size and stay there.
Read more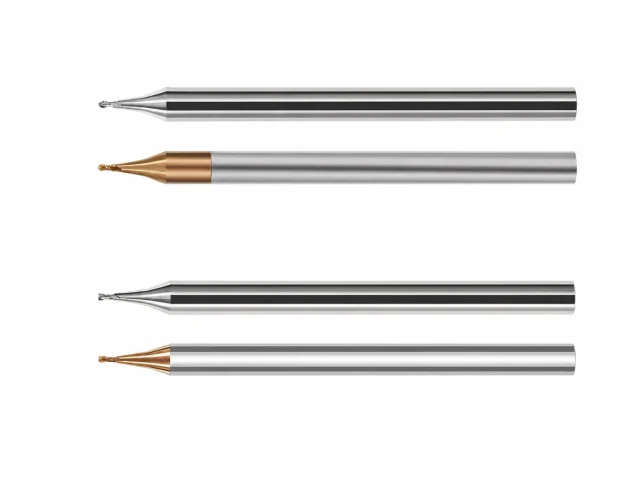
Straight-flute H7 reaming for through holes, at a price that makes sense for general production.
Read more
Spiral flutes push the chip ahead of the cut, so a blind hole does not get scored on the way in.
Read moreMost of what we ship is ground to a drawing. Send yours — we quote within 24 hours.