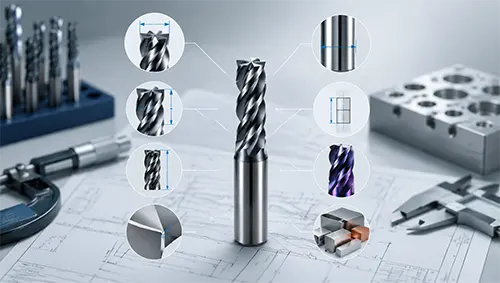
Cutting Data Basics: Starting Parameters for 4-Flute Carbide End Mills
Surface speed, chip load and the two adjustments that fix most cuts. A no-nonsense starting table for 4-flute solid carbide tools.

Cutting data fails in the field for two reasons: it is quoted for ideal conditions, or it is adjusted in the wrong order. This is the starting table we ship with our 4-flute tools, plus the adjustment sequence that gets from “catalog number” to “runs on your machine”.
Starting points, 12 mm · 4-flute · rigid setup
| Operation | Steel (45#) | 304 stainless | 6061 aluminium |
|---|---|---|---|
| Side milling, ap 1×D | 150 m/min · 0.060 mm/z | 120 m/min · 0.045 mm/z | 500 m/min · 0.080 mm/z |
| Finishing, ae 0.05×D | 200 m/min · 0.040 mm/z | 180 m/min · 0.030 mm/z | 800 m/min · 0.050 mm/z |
| Full slot, ap 0.5×D | 110 m/min · 0.045 mm/z | 90 m/min · 0.035 mm/z | 350 m/min · 0.060 mm/z |
| Trochoidal / dynamic | 220 m/min · 0.070 mm/z | 200 m/min · 0.060 mm/z | 900 m/min · 0.100 mm/z |
Convert to RPM and feed correctly
RPM = (surface speed × 1000) ÷ (π × diameter). Table feed = RPM × flutes × chip load. For a 12 mm tool at 120 m/min: RPM ≈ 3,183, feed ≈ 570 mm/min at 0.045 mm/z. If your machine cannot hold the RPM, hold the chip load and accept the surface speed you can get — then adjust coolant, not courage.
The adjustment sequence that works
- Chips tell you before the tool does. Silver-gray, warm chips: correct. Blue chips with good tool life: fine. Blue chips and rapid edge wear: drop surface speed 20%.
- Adjust speed first for wear, feed first for finish. Edge rounding and cratering are speed problems. Smearing and rubbing are feed problems.
- Reduce for reach. Over 3×D reach, cut the table values 20%; over 5×D, 40% and expect to re-prove the cut.
- Prove the first part at 80%. Ramp to full parameters across the first ten parts, watching spindle load, not just the sound.
When the table is not enough
Thin walls, interrupted cuts, long overhangs and mixed stock all shift the window. That is why every Conko order can ship with parameters for your actual operation — tell us the setup and the data sheet comes with the quotation, not after the first broken tool.