
About this tool
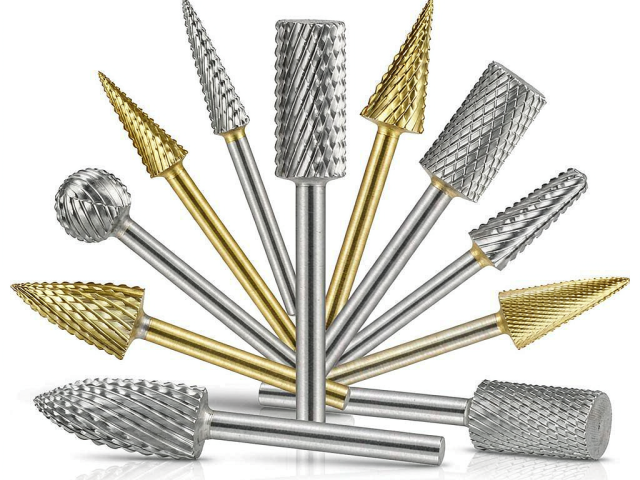
The double-cut burr is the one that ends up in everybody die grinder: cross teeth that break the chip, a finish usually good enough to stop there, and a brazed shank that takes the side load of dressing a weld.
Where it works
Deburring, chamfering, weld dressing and light stock removal in steel, stainless and cast iron.
Cutting data — starting point
Starting values for a rigid setup with a good coolant supply. Treat them as a first trial, then adjust to the machine, the holder and the actual condition of the material.
| Work material | Cutting speed vc | Feed | Depth of cut |
|---|---|---|---|
| Steel / stainless (P/M) | 15,000–25,000 rpm | Hand feed | Light, steady pressure |
| Cast iron (K) | 15,000–25,000 rpm | Hand feed | Light, steady pressure |
| Hardened steel (H) | 10,000–18,000 rpm | Hand feed | Light pressure, no dwell |
What you can specify
- Diameter, corner radius and flute count ground to your drawing
- Coating — AlCrN, AlTiN, TiAlN, DLC or uncoated, matched to the workpiece
- Shank — h6 ground, HA / HB / whistle-notch
- Laser-marked part number, or blank shanks for distributor stock
Not sure about the geometry? Send the drawing or a photo of the part. We recommend the profile, the coating and the starting cutting data — and quote from there.