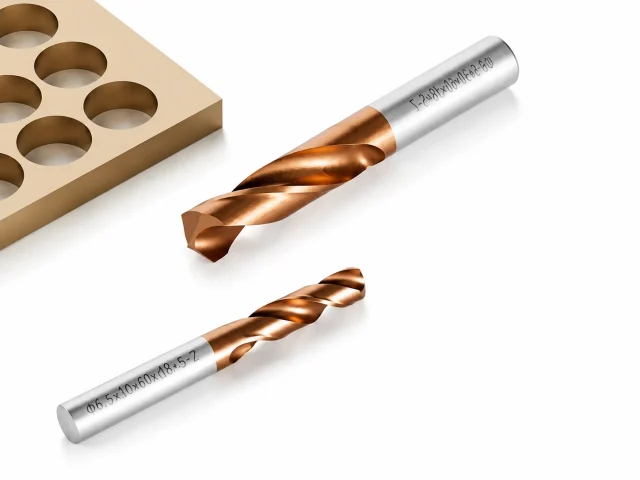
About this tool
Micro drills break for reasons that are rarely the drill, but runout, deflection or a wandering start. Tight runout tolerances and a reinforced web remove most of that, and a sharp point means you can usually skip the center drill.
Where it works
Small holes in steel, stainless and aluminium: fuel and hydraulic components, medical parts and connector work.
Cutting data — starting point
Starting values for a rigid setup with a good coolant supply. Treat them as a first trial, then adjust to the machine, the holder and the actual condition of the material.
| Work material | Cutting speed vc | Feed | Depth of cut |
|---|---|---|---|
| Steel (P) | 60–120 m/min | 0.03–0.08 mm/rev | 2×D |
| Stainless (M) | 40–80 m/min | 0.02–0.06 mm/rev | 1.5×D |
| Aluminium (N) | 120–250 m/min | 0.04–0.10 mm/rev | 3×D |
What you can specify
- Diameter, corner radius and flute count ground to your drawing
- Coating — AlCrN, AlTiN, TiAlN, DLC or uncoated, matched to the workpiece
- Shank — h6 ground, HA / HB / whistle-notch
- Laser-marked part number, or blank shanks for distributor stock
Not sure about the geometry? Send the drawing or a photo of the part. We recommend the profile, the coating and the starting cutting data — and quote from there.