About this tool
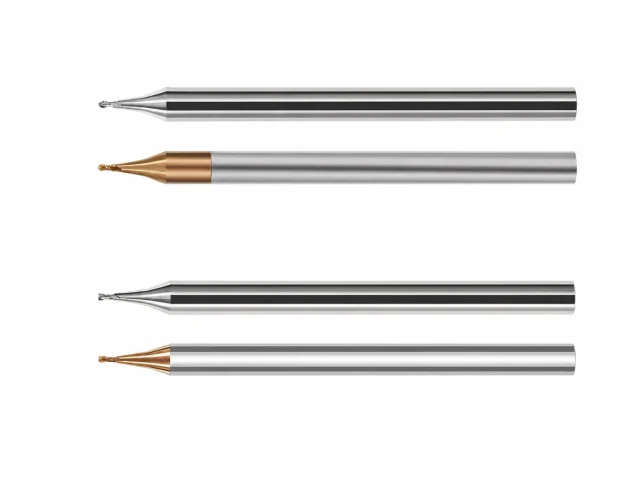
At this size the tool is only as good as its runout. A micron of eccentricity is a meaningful fraction of a Ø0.2 mm edge, so these are ground and inspected on dedicated micro machines and shipped with the runout figure on the label.
Where it works
Connector molds, medical components, watch parts and any feature that a Ø1 mm tool cannot enter.
Cutting data — starting point
Starting values for a rigid setup with a good coolant supply. Treat them as a first trial, then adjust to the machine, the holder and the actual condition of the material.
| Work material | Cutting speed vc | Feed | Depth of cut |
|---|---|---|---|
| Steel (P) | 100–180 m/min | 0.005–0.015 mm/tooth | 0.05×D |
| Aluminium (N) | 200–400 m/min | 0.010–0.030 mm/tooth | 0.1×D |
| Copper / brass (N) | 150–300 m/min | 0.010–0.030 mm/tooth | 0.1×D |
What you can specify
- Diameter, corner radius and flute count ground to your drawing
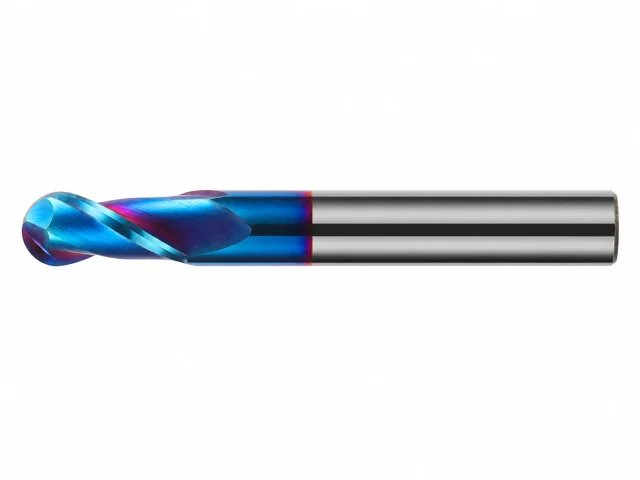
- Coating — AlCrN, AlTiN, TiAlN, DLC or uncoated, matched to the workpiece
- Shank — h6 ground, HA / HB / whistle-notch
- Laser-marked part number, or blank shanks for distributor stock
Not sure about the geometry? Send the drawing or a photo of the part. We recommend the profile, the coating and the starting cutting data — and quote from there.