About this tool
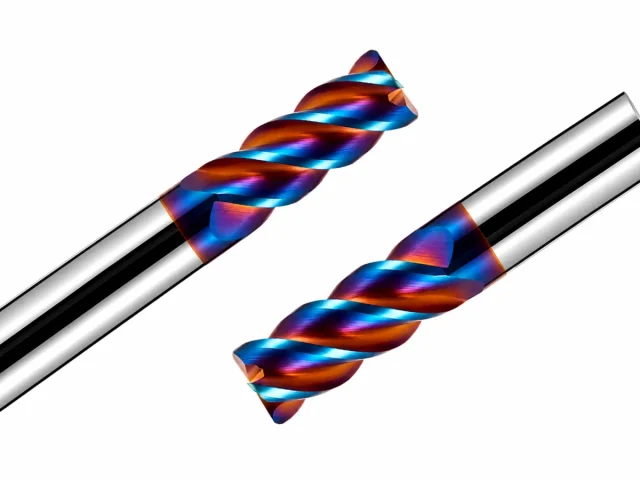
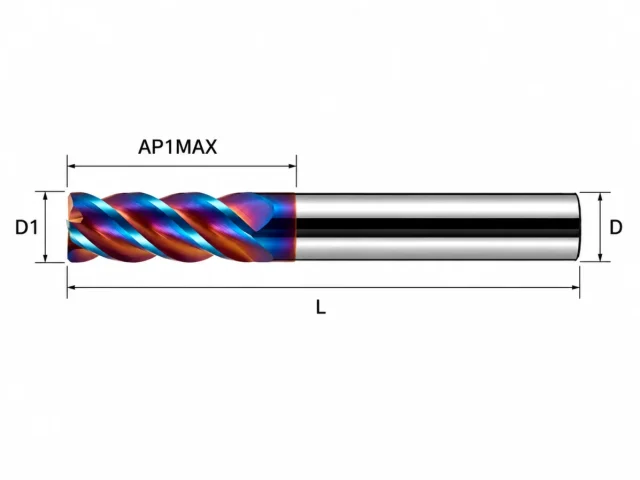
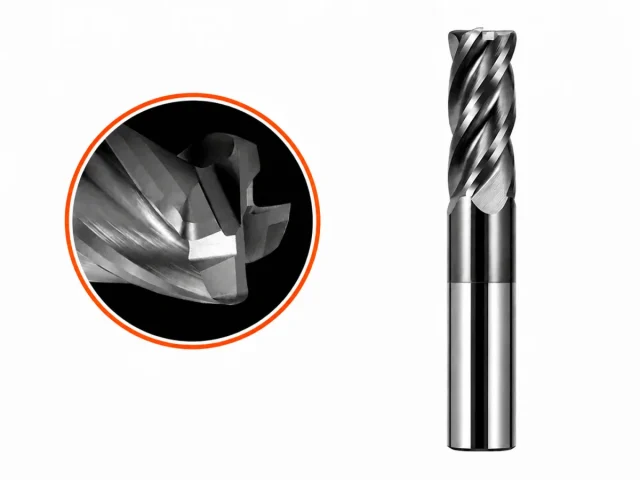
A four-flute square end mill that covers most of what a job shop does in a week: slotting, shoulder milling, pocketing and finishing. The 38° helix and a sub-micron carbide substrate give it a wide working window, and the AlCrN coating lets it run dry or with minimum lubrication without giving up tool life.
Where it works
Steel, cast iron and stainless at moderate to high cutting speeds. A good first choice where the setup is rigid and the operation changes from part to part.
Cutting data — starting point
Starting values for a rigid setup with a good coolant supply. Treat them as a first trial, then adjust to the machine, the holder and the actual condition of the material.
| Work material | Cutting speed vc | Feed | Depth of cut |
|---|---|---|---|
| Carbon steel (P) | 180–260 m/min | 0.03–0.06 mm/tooth | 0.5×D |
| Stainless (M) | 90–140 m/min | 0.02–0.04 mm/tooth | 0.3×D |
| Cast iron (K) | 150–220 m/min | 0.03–0.05 mm/tooth | 0.4×D |
| Hardened steel 45–55 HRC (H) | 70–110 m/min | 0.015–0.03 mm/tooth | 0.2×D |
What you can specify
- Diameter, corner radius and flute count ground to your drawing
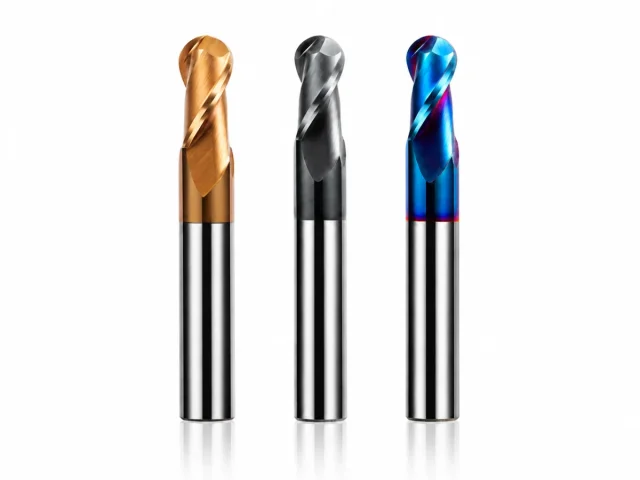
- Coating — AlCrN, AlTiN, TiAlN, DLC or uncoated, matched to the workpiece
- Shank — h6 ground, HA / HB / whistle-notch
- Laser-marked part number, or blank shanks for distributor stock
Not sure about the geometry? Send the drawing or a photo of the part. We recommend the profile, the coating and the starting cutting data — and quote from there.