
Solutions by industry
Start from the material, the machine and the operation — not from page one of a catalog. Each route pairs a recommended tool geometry with starting cutting data.

3-Flute Corner Radius End Mill — Aluminium
High-helix three-flute geometry with a radiused corner for aluminium, where chip clearance decides the finish.
Read more
Micro End Mill — DLC Coated, Aluminium
Diamond-like carbon on a micro edge: the coating that stops aluminium sticking where you cannot afford to stop and clean the tool.
Read more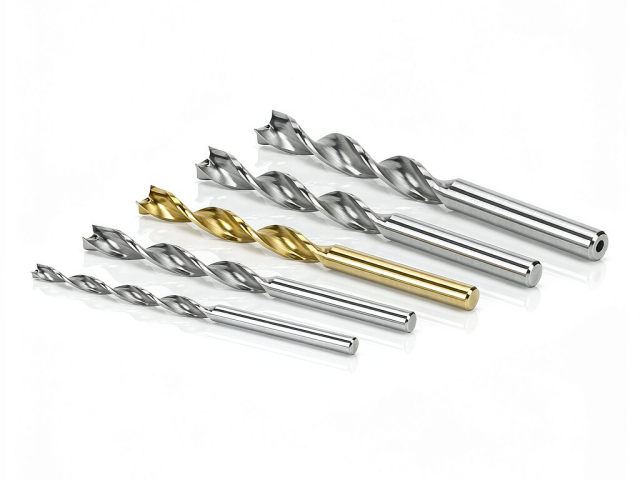
Solid Carbide Drill — Aluminium, Polished Flute
Polished flutes and a wide helix for aluminium: chips leave fast, and the hole comes out on size.
Read more
Carbide Burr — Aluminium Cut, Single Flute
A single-flute alu-cut geometry that clears soft chips without loading up the teeth.
Read more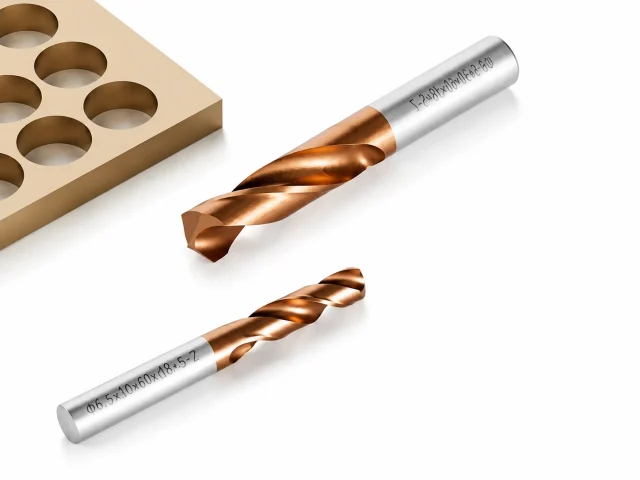
Special Geometry End Mill — Aerospace Alloys
Geometry developed for titanium and superalloys: controlled rake, reinforced edges and clearance that keeps heat out of the cut.
Read more
3-Flute Square End Mill — Aluminium
Polished three-flute geometry with a high helix, built for aluminium and non-ferrous work at high spindle speeds.
Read more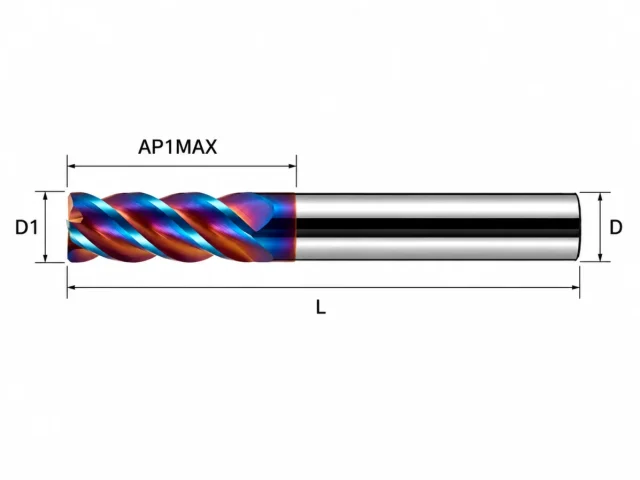
5-Flute Variable Helix Square End Mill — Stainless
Variable helix and unequal flute spacing break the harmonics that make stainless steel ring. Quieter, and noticeably longer tool life.
Read more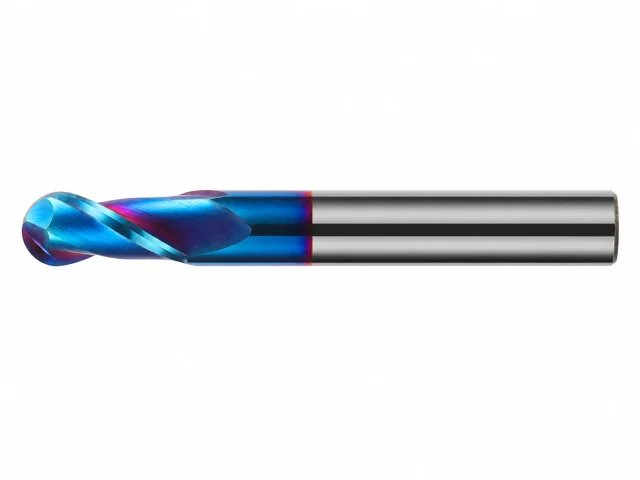
Ball Nose End Mill — Deep Cavity, 4-Flute
Neck relief and a four-flute core for cavities deeper than three diameters, where chip evacuation and stiffness both matter.
Read more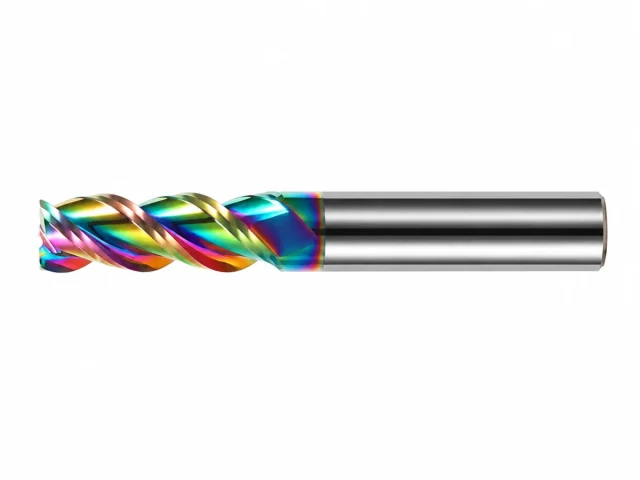
2-Flute Ball Nose End Mill — Long Reach
A long, slender ball nose for deep cavities and radii that sit well below the surface line, with a tapered neck for rigidity.
Read moreCan't find the geometry you need?
Most of what we ship is ground to a drawing. Send yours — we quote within 24 hours.